
Food and Beverage PLC Spare Parts Planning Guide
Plan food and beverage automation spares around batch risk, washdown conditions, PLCs, sensors, drives, networks, backups, and recovery tests.
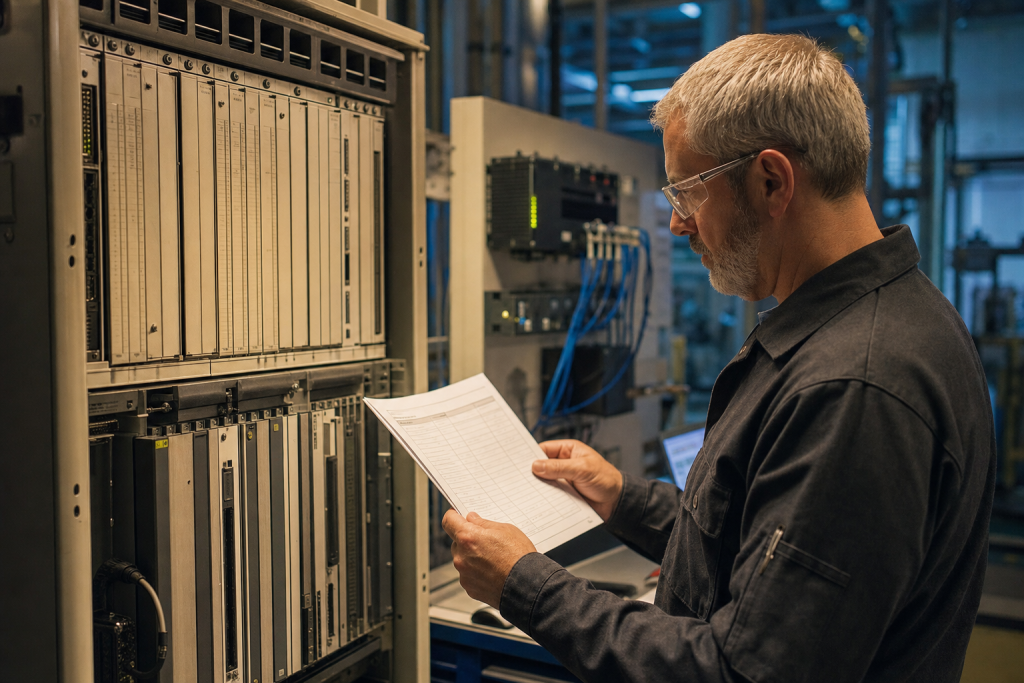
In food and beverage plants, an automation failure can damage more than production output. A stopped filler, mixer, conveyor, pasteurizer, dosing skid, or packaging line may also interrupt a batch, create cleaning work, affect traceability, and compress the time available for quality decisions. A useful spare plan must therefore connect the control hardware to the process and compliance consequences around it.
The right question is not simply “Do we have a spare PLC?” It is “Can we restore the control path, prove the process is behaving correctly, and return to production without losing the evidence operators and quality teams need?”
Map the line and the batch consequence
Start with the production areas that can stop or compromise a batch: ingredient handling, weighing, mixing, cooking, pasteurization, filling, capping, labeling, inspection, refrigeration, cleaning-in-place, wastewater, and packaging. Record which controller, remote I/O station, HMI, drive, instrument, network, and power supply serves each area.
Then record the consequence of losing automatic control, losing a critical measurement, or losing the operator interface. A short stoppage on a conveyor may be recoverable, while a temperature or dosing control failure can force a batch review or disposal. The priority should follow the process consequence, not the purchase price of the module.
Use the PLC and controller collection to organize the controller portion of the inventory. For each installed model, record revision, firmware, rack position, I/O arrangement, application backup, and the recovery procedure required by the maintenance team.
Account for washdown and hygienic environments
Food and beverage equipment can face water, cleaning chemicals, temperature changes, vibration, condensation, and frequent maintenance access. The spare register should record enclosure conditions, ingress protection, connector sealing, cable glands, mounting requirements, and storage controls.
Do not assume that a visually similar sensor or connector is suitable for a washdown area. Check the process connection, wetted materials, signal type, temperature range, hygienic requirements, calibration method, and the way the measurement is used in control and alarm logic.
The industrial sensors collection can support category planning, but the installed measurement chain remains the authority. Record the transmitter, cable, scaling, alarm limits, calibration evidence, and any spare accessories needed to complete the loop.
Protect drives, motors, and packaging machines
Many line failures are caused by an automation dependency outside the PLC cabinet. Conveyors, pumps, fans, fillers, cappers, mixers, and refrigeration equipment may use variable-frequency drives, servo systems, soft starters, or packaged controllers.
For each drive or motion device, capture motor data, parameter backup, communication interface, local/remote settings, speed reference, feedback, permissives, braking or bypass arrangements, and the safe restart sequence. A replacement drive that powers up but lacks its application parameters is not a ready spare.
Review variable-frequency inverter coverage and servo motor and drive coverage as part of the same recovery path. Food lines often have tight changeover windows, so parameter files, cables, connectors, and commissioning steps should be stored with the spare record.
Keep traceability and operator visibility in the plan
An automation recovery may be technically successful but still incomplete if batch records, alarms, recipes, historian tags, or inspection signals are missing. Record the HMI project, recipe data, alarm configuration, historian mapping, user roles, time synchronization, and report requirements that must be restored.
For quality-sensitive processes, define what operators and quality personnel must verify before product is released. This may include temperature profiles, dosing totals, pressure, fill level, metal detection, checkweigher results, cleaning status, or the continuity of electronic records. The exact checks vary by process, so document them with the site team rather than inventing a generic acceptance test.
Include network and power dependencies
Identify Ethernet, fieldbus, remote I/O, managed switches, media converters, wireless gateways, and plant-level interfaces. Record topology, addressing, redundancy, configuration backup, and the local operating mode if the control room connection is lost.
Power supplies, redundancy modules, breakers, and control transformers can affect several line sections at once. Note input and output ratings, shared loads, alarm contacts, terminal arrangements, and the safe isolation method. A controller spare cannot restore a line if the supporting power or network path is unavailable.
Build a recovery test around the production window
Before a spare is classified as ready, define a staged test. It may include controller startup, project restoration, I/O diagnostics, simulated analog values, drive communications, HMI screens, recipe access, alarm routing, historian tags, time synchronization, and loss-of-communications behavior.
For a batch process, include the handoff from maintenance to operations and quality. Confirm how the line returns from manual control to automatic control, how an interrupted batch is handled, and which readings must be checked before production resumes. Keep evidence with the spare: model photographs, firmware, configuration version, test date, limitations, and approver.
Create a food and beverage RFQ
Include the exact model, installed quantity, spare quantity, condition requirement, destination, required date, process unit, and consequence of delay. Attach label photos, cabinet views, connector details, firmware information, parameter backups, and the planned maintenance window.
Ask for separate options for exact-model supply, tested repair or exchange, compatible alternative, and longer-term modernization. Request inspection scope, test evidence, warranty, traceability, packaging, and any limitations relevant to washdown or hygienic service.
FAQ
How many PLC spares should a food plant keep?
Use line criticality, batch consequence, installed population, shared dependencies, repair time, lifecycle status, and the ability to operate manually. A common low-risk input card may need less coverage than a controller or dosing interface.
Is a spare sensor enough if the PLC is healthy?
Not always. Scaling, calibration, wiring, transmitter settings, alarm limits, process connection, and quality acceptance checks may all be required before the measurement can support production.
What should be backed up for a packaging line?
Back up the PLC and HMI applications, recipes, drive and motion parameters, network configuration, alarm settings, historian tags, and the engineering-tool versions needed to restore them.
Should refurbished drives or PLCs be accepted?
They can be considered when condition, inspection scope, test evidence, warranty, traceability, and application verification are agreed before purchase. Keep refurbished, repaired, surplus, and untested statuses separate.
Make the spare plan usable during a line stop
SmartNexMSK can help organize food and beverage model lists, label evidence, sensor and drive dependencies, configuration questions, and delivery targets. Send model numbers, photos, quantity, destination, and the required maintenance window to [email protected] or WhatsApp/Phone +86 18259474341.
Route this topic into a sourcing request
Connect the article topic to a model number, category, brand, quantity, and destination before opening the RFQ.
Related Insights
Continue with sourcing and model matching guides
 Sep 8, 2026
SANYO DENKI QS1E Spares: Save Parameters First
When a SANMOTION Q axis stops, the purchasing request often becomes a model number: “Please quote QS1E01AA0H4A3P1T.” That is a useful starting point, but…
Read guide Sep 6, 2026
Yaskawa SGDH-05DE-OY Spares: Check the Servo Chain
A servo drive fault often produces a deceptively simple purchasing request: “Replace the SGDH-05DE-OY.” In a running machine, however, the amplifier is only one…
Read guide Sep 5, 2026
GE IS220PCLAH1A Spares: Check Mark VIe Fit
When a Mark VIe cabinet develops an intermittent control fault, the urgent request often becomes a single line: “Please quote IS220PCLAH1A.” That is understandable…
Read guide