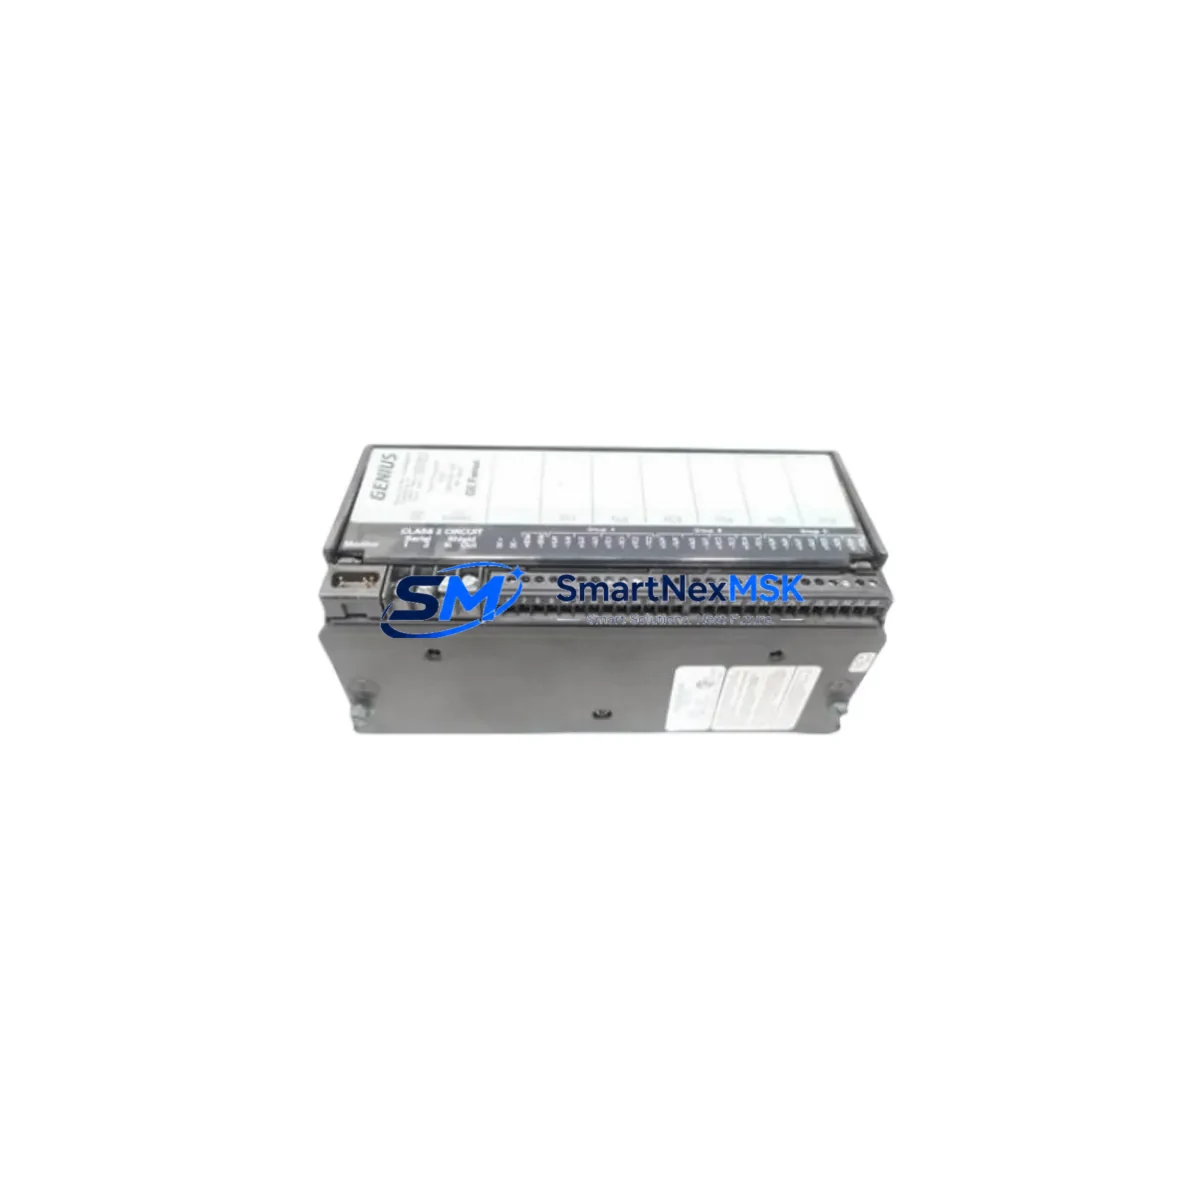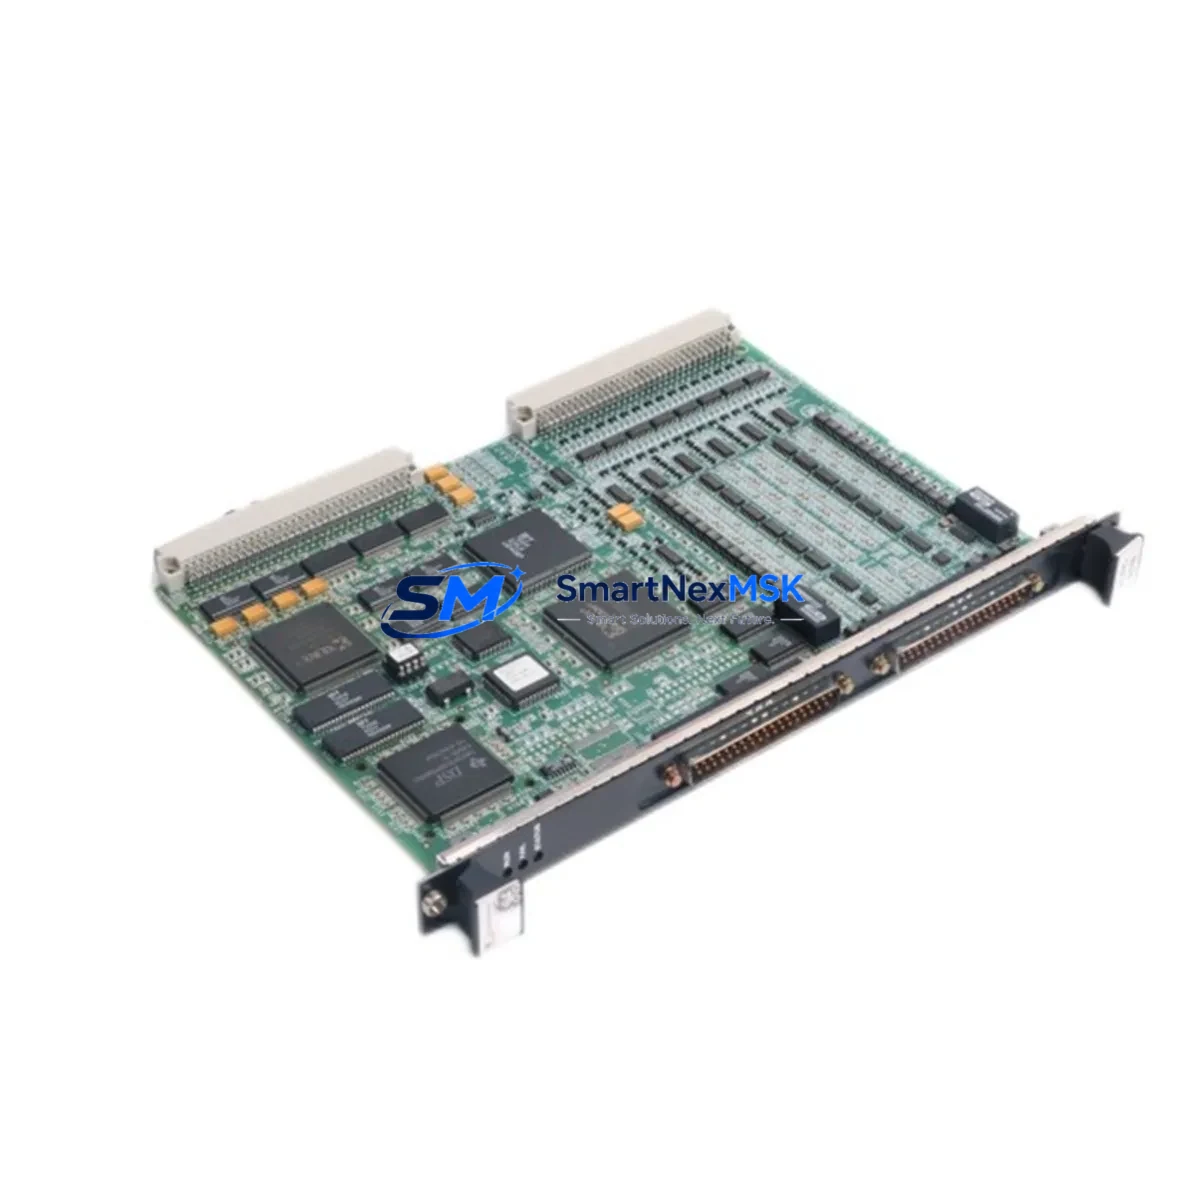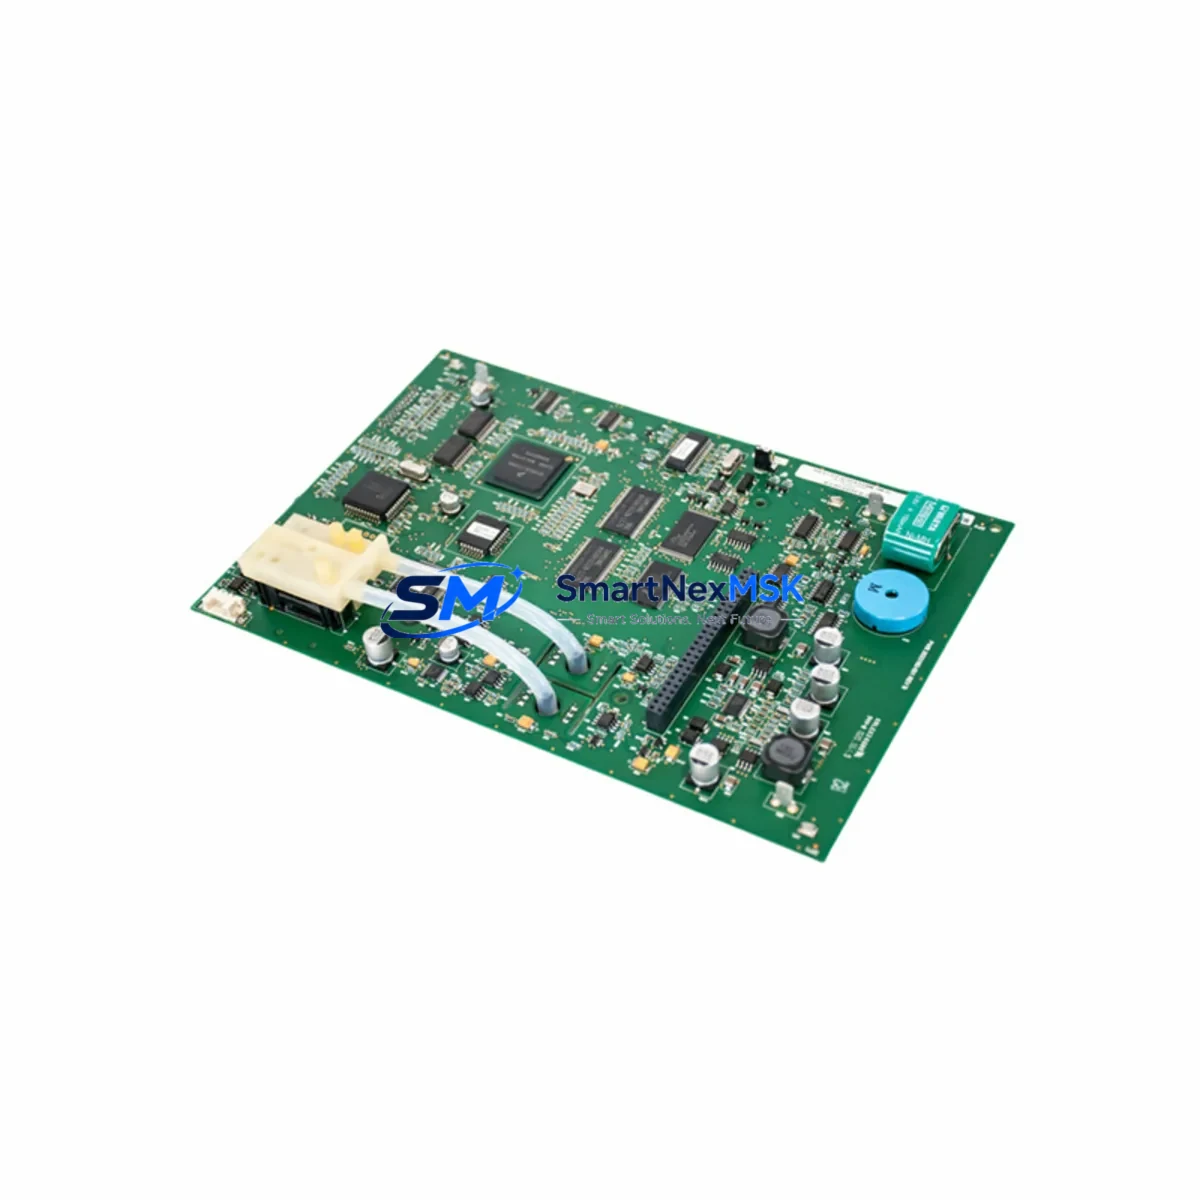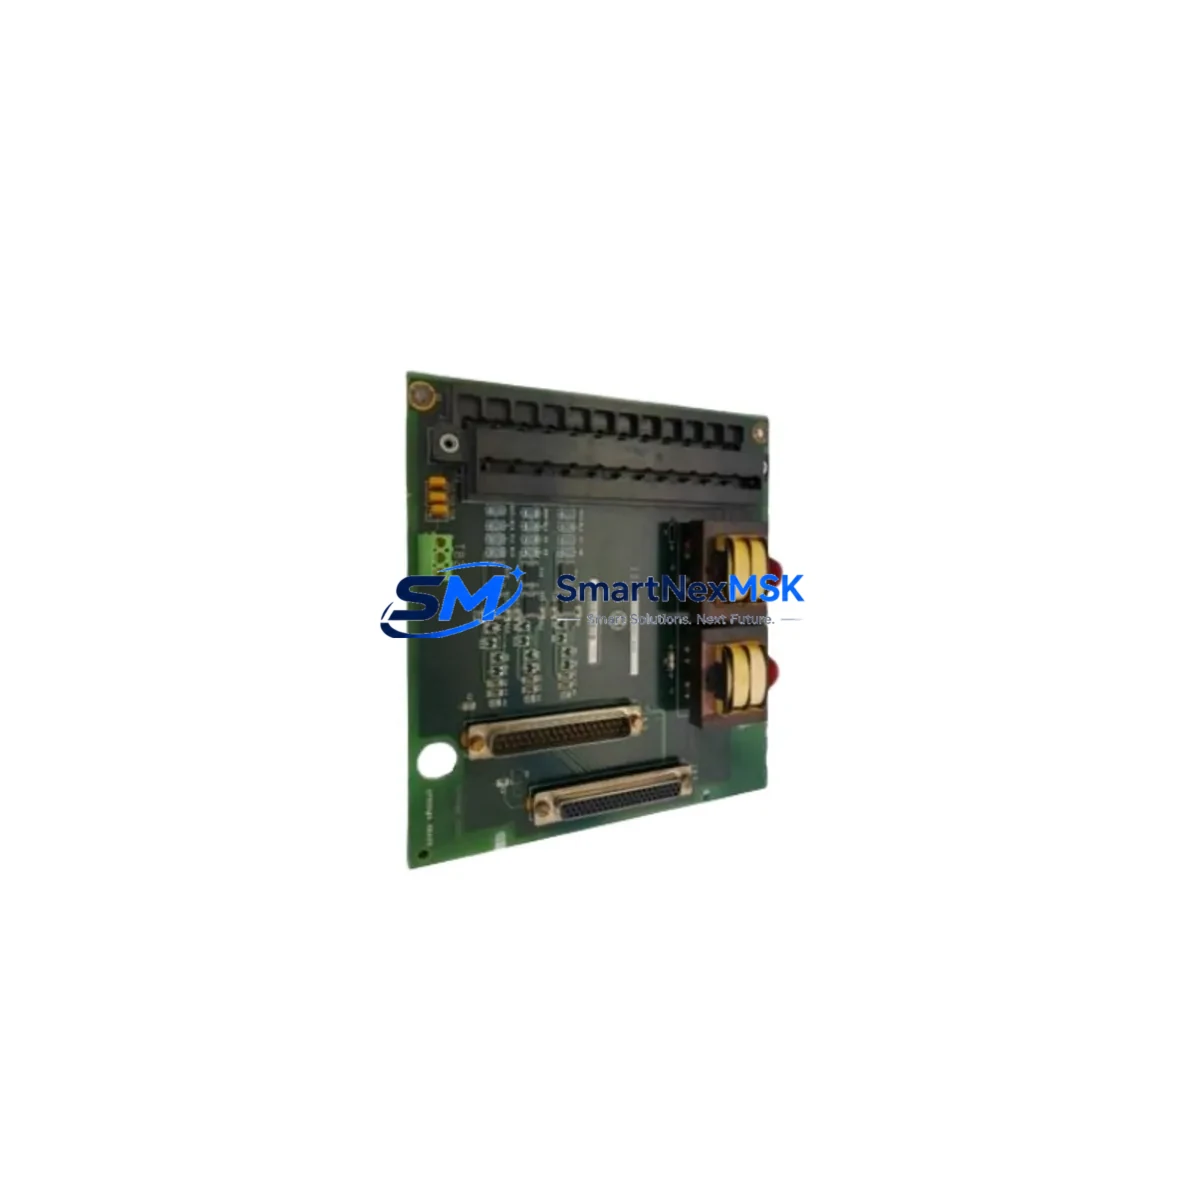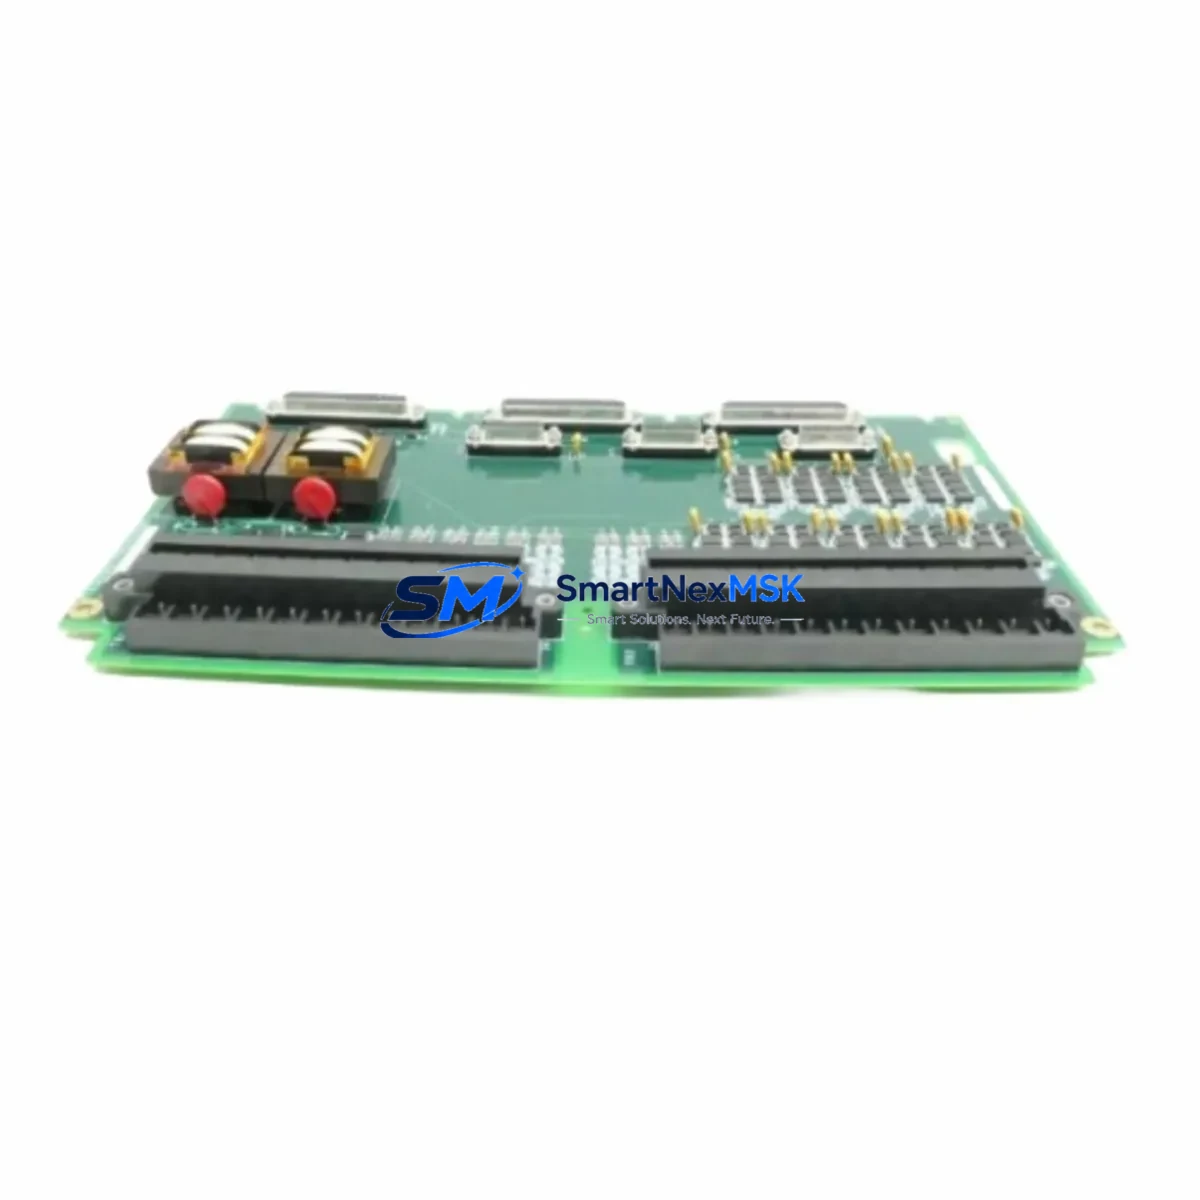
GE IS200TPROH1BBB Retrofit-Ready Processor Card for Mark VI Control Systems
The GE IS200TPROH1BBB is a high-reliability processor card engineered for the GE Mark VI turbine control platform. As legacy Mark V and early Mark VI installations reach end-of-support milestones, plant engineers and control system integrators increasingly rely on verified replacement units like the IS200TPROH1BBB to sustain operational continuity without committing to a full DCS overhaul. This card serves as a direct retrofit solution for aging processor assemblies, enabling smooth migration paths that protect existing I/O wiring, backplane architecture, and ladder logic investments.
Whether you are managing a gas turbine, steam turbine, or combined-cycle plant, the IS200TPROH1BBB slots into the Mark VI control cabinet with minimal re-engineering. Its compatibility with the standard Mark VI VME backplane means that adjacent modules — including the IS200VCRCH1B VME crate controller, IS200DSPXH1B digital signal processor, and IS200BICLH1B I/O link controller — remain undisturbed during the swap. This dramatically reduces the scope of a planned outage and limits the risk of cascading configuration changes across the control network.
Upgrade Compatibility Table
| Parameter | Details |
|---|---|
| Compatible Platform | GE Mark VI Turbine Control System |
| Replaces / Upgrades | IS200TPROH1AAA, IS200TPROH1BAA, IS200TPROH1BAB (earlier hardware revisions) |
| Backplane Interface | VME 6U standard; compatible with Mark VI VCRC and VCRCH crate controllers |
| Communication Compatibility | IONET (GE proprietary), Ethernet (100Base-T), serial RS-232/RS-485 |
| Installation Requirement | Verify slot address assignment in ToolboxST before insertion; match existing I/O pack addressing |
| Firmware Consideration | Confirm ToolboxST project firmware revision matches card hardware revision suffix (BBB) |
| Replacement Recommendation | Direct drop-in for same-suffix units; cross-revision replacement requires ToolboxST re-download |
| Commissioning Focus | Re-validate IONET node address, confirm watchdog timer response, verify I/O pack health status in HMI |
| Warranty | 12 months from date of shipment; covers manufacturing defects and functional failure |
Retrofit Planning for Existing Automation Systems
A successful IS200TPROH1BBB retrofit begins well before the card arrives on site. The first step is a thorough audit of the existing Mark VI cabinet layout. Identify the current processor card revision, document the VME slot assignments, and photograph all terminal block wiring on adjacent I/O packs such as the IS200TBCIH1B terminal board and any connected IS200TBAIH1B analog input terminal assemblies. This documentation becomes the baseline for post-swap verification.
Power supply capacity is a critical pre-check. The Mark VI cabinet typically uses a IS200EPCTG1A or equivalent 28 VDC power supply module. Confirm that the existing supply can sustain the processor card’s inrush current during boot-up, particularly if additional I/O expansion cards have been added to the crate since the original commissioning. Overloaded power rails are a common root cause of intermittent processor faults that are misdiagnosed as card failures.
Communication link integrity must be validated before and after the swap. The IS200TPROH1BBB communicates with the HMI workstation via IONET and Ethernet. If the plant is running an older Cimplicity HMI version, verify that the ToolboxST project file is backed up and that the HMI screen database references the correct controller node name. A node name mismatch after a processor replacement is one of the most common causes of post-swap alarm floods and false trip signals.
For plants that have already migrated portions of their control architecture to newer platforms, the IS200TPROH1BBB can coexist in a hybrid environment alongside IS200STCIH1B servo terminal boards and IS200VSVOH1B vibration monitoring modules. This makes it an ideal bridge component during phased upgrades where full platform replacement is deferred to a future outage window. The card’s support for both legacy serial protocols and modern Ethernet-based diagnostics ensures it can interface with updated SCADA layers without requiring a full I/O rewire.
Before closing the cabinet, verify the backplane connector seating, confirm that all VME card ejector levers are fully engaged, and perform a continuity check on the IONET fiber connections if applicable. A pre-power-up checklist that includes these steps reduces the risk of a second unplanned outage caused by a loose connection rather than a component fault.
Downtime Control During System Migration
Minimizing downtime during a Mark VI processor card replacement requires a structured hot-swap protocol and a pre-staged spare strategy. Begin by placing the turbine in a controlled hold state and transferring supervisory control to a redundant controller if the system is configured in dual-redundant mode. The IS200TPROH1BBB supports the Mark VI redundancy architecture, meaning that in a properly configured dual-processor setup, the standby card can assume control while the primary is replaced — reducing the actual process interruption to the time required for a controlled switchover rather than a full shutdown.
Before pulling the failed card, use ToolboxST to export the current controller configuration, including all I/O pack assignments, setpoint values, and alarm limits. Store this export on an isolated engineering workstation — not on the HMI server — to prevent accidental overwrite. Once the IS200TPROH1BBB is seated and powered, perform a fresh ToolboxST download to the card and verify that all I/O pack health indicators return to normal status within the expected boot cycle time (typically under 90 seconds for a standard Mark VI configuration).
Post-swap, run a full functional test sequence: verify analog input scaling on critical process variables, confirm digital output response on trip solenoids, and validate that the HMI alarm summary reflects the correct controller status. If the plant uses a GE WorkstationST or third-party SCADA system for data historian integration, confirm that the OPC-DA or OPC-UA data path re-establishes automatically after the controller reboot. Document the as-found and as-left configuration states for the maintenance record and regulatory compliance file.
Retrofit Support FAQ
Q1: Is the IS200TPROH1BBB a direct replacement for IS200TPROH1AAA or IS200TPROH1BAA?
The BBB hardware revision is functionally compatible with earlier AAA and BAA revisions in most Mark VI configurations. However, a ToolboxST firmware re-download is recommended when crossing hardware revision boundaries to ensure the firmware image matches the card’s hardware capabilities. Confirm the ToolboxST project revision level before proceeding.
Q2: What wiring changes are required during installation?
No wiring changes are required at the terminal board level. The IS200TPROH1BBB connects to the system via the VME backplane, not via direct field wiring. All field terminations remain on the I/O terminal boards (e.g., IS200TBCIH1B, IS200TBAIH1B) and are unaffected by the processor card swap. Only the VME backplane connector and IONET/Ethernet cables need to be reseated.
Q3: How is compatibility verified before shipment?
Each IS200TPROH1BBB unit undergoes a bench-level functional test prior to shipment, including power-on self-test (POST) verification, VME bus communication check, and Ethernet port validation. A test report is available upon request. Units are shipped with ESD-protective packaging and include a 12-month warranty covering manufacturing defects and functional failure under normal operating conditions.
Q4: What support is available for on-site commissioning and debugging?
Our technical team provides pre-shipment configuration consultation, including review of your ToolboxST project file for known compatibility issues. Post-delivery, we offer remote commissioning support via email and phone to assist with node address configuration, firmware download procedures, and I/O pack health verification. Contact our team at [email protected] or +86 18259474341 for project-specific support.
© 2026 SMARTNEXMSK. All rights reserved.
Original Source: https://smartnexmsk.com
Contact: [email protected] | +86 18259474341