
How to Validate Refurbished PLC Spares Before Installation
Use a practical receiving and test checklist to verify refurbished PLC spares, protect compatibility, and reduce commissioning risk before installation.
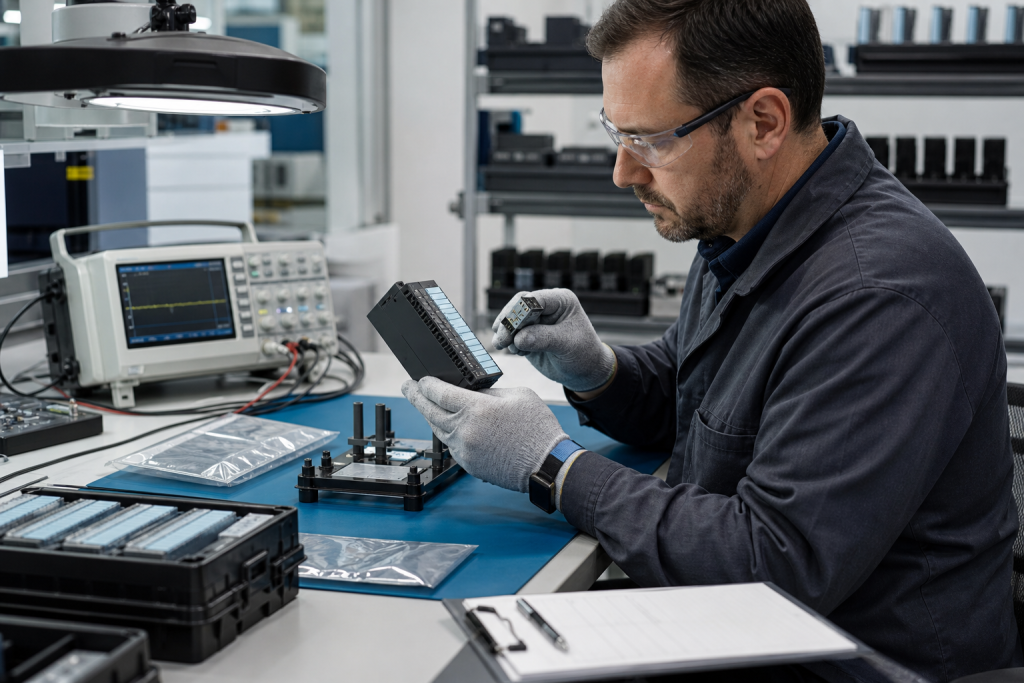
A refurbished PLC module can be a sensible way to protect an aging control system, especially when an exact model is no longer produced or an OEM lead time does not fit the maintenance window. The risk appears when “refurbished,” “tested,” and “ready for service” are treated as the same statement. They are not.
A receiving technician should be able to answer three separate questions before a spare reaches a live rack: Is this the exact unit that was ordered? Has its physical and electrical condition been checked? Has its compatibility with the installed application been established? A power-on test can help, but by itself it does not prove that the module will run the site’s firmware, configuration, I/O load, network path, or safety process correctly.
Start with identity and traceability
The first control is a model-identity check. Compare the part number, series, revision, suffix, voltage, channel count, connector arrangement, and any firmware or hardware identifier against the approved request. Record the serial number and photograph the label before the unit is moved into storage.
This matters because a product family can contain modules that look almost identical while carrying different electrical ratings, terminal assignments, firmware requirements, or controller compatibility. For an Allen-Bradley 1756-L81E ControlLogix controller spare, for example, the exact controller revision and installed firmware context are more useful than a general statement that the unit is “ControlLogix compatible.”
Keep the supplier’s packing list, test report, repair notes, warranty terms, and photographs with the receiving record. If a unit has been repaired, ask what was replaced and what was tested. If the seller cannot define the inspection scope, mark the item as unverified rather than upgrading it to “ready.”
Inspect the physical condition before applying power
Use a clean ESD-safe bench and inspect the module before connecting it to a test rack. Look for damaged housings, bent pins, cracked terminal blocks, corrosion, contamination, missing labels, broken seals, heat discoloration, loose hardware, and evidence of previous moisture or improper storage.
Inspect the connector face and the mating interface separately. A module can appear clean while carrying damaged contacts or a distorted guide that prevents a reliable connection. Check removable terminal blocks, battery compartments, memory media, keying, mounting clips, and backplane guides. Photograph anything that differs from the approved receiving condition.
Separate a power-on test from a functional test
A power-on test answers a narrow question: does the device start without an immediate fault? A functional test should answer more. The right test depends on the module, but a controlled checklist may include:
- Correct rack, backplane, power, and grounding conditions.
- Expected startup behavior, diagnostic indicators, and fault codes.
- Firmware or operating-system identification and revision capture.
- Input and output channel checks using safe test signals or a simulator.
- Communication, addressing, and network behavior where applicable.
- Retention of configuration, calibration, and diagnostic evidence.
Do not connect a spare directly to a live process merely to discover whether it works. Use a representative test rack, a documented simulator, or an approved offline environment whenever possible. For safety-related or process-critical equipment, the test must follow the site’s engineering, change-control, and functional-safety requirements.
Compatibility is more than the connector
Mechanical fit is only one layer of compatibility. Check the controller family, firmware range, project file, I/O map, parameter set, communication protocol, power arrangement, network topology, and application role. A module may pass a bench test and still be unsuitable because the installed controller cannot accept its revision or the project cannot be restored.
Review related communication modules and I/O hardware when the spare is part of a distributed control path. A replacement I/O module can depend on a fieldbus coupler, remote adapter, network switch, termination arrangement, or HMI mapping that is not visible from the module label. The receiving record should identify those dependencies before the spare is approved.
For a mixed or aging cabinet, a broader industrial PLC and controller sourcing review can help organize the surrounding assets. It should not be used to assume interchangeability. Each replacement decision still needs a model-specific comparison and an approved commissioning plan.
Use a clear condition vocabulary
Procurement and maintenance teams need shared definitions. “New old stock,” “surplus,” “refurbished,” “repaired,” “exchange,” and “as-is” describe different evidence levels. The exact definitions can vary by supplier, so write the required condition into the RFQ and purchase record.
A practical internal status system might include:
- Received: identity and packaging recorded; functional status not yet approved.
- Inspected: physical condition and model evidence checked.
- Bench-tested: the defined electrical or diagnostic test passed.
- Application-verified: firmware, configuration, and interface compatibility reviewed.
- Outage-ready: the spare has an owner, location, evidence package, and approved replacement procedure.
This vocabulary prevents a tested unit from being mistaken for a fully deployable spare. It also makes shelf audits more useful because the team can see which items still need application verification.
Build the RFQ around evidence
A good RFQ includes the exact model, revision, quantity, installed application, condition requirement, destination, required date, and whether the part is for emergency recovery or planned inventory. Add label photographs, cabinet context, connector views, current fault symptoms, firmware information, and the available configuration backup.
Ask for separate options when appropriate: exact model, repaired unit, exchange unit, compatible alternative, and a longer-term replacement route. Request the test scope, warranty, traceability, packaging, and limitations. A lower price is not a lower risk if the buyer cannot tell what was actually tested.
An exact product page such as an ABB AC500 automation spare can make the model-specific request clearer, but the buyer still needs to provide site evidence. The page identifies the sourcing target; the installed system determines whether the target is usable.
FAQ
Is a refurbished PLC spare safe if it powers on?
Not necessarily. Power-on proves only that the unit starts under the test conditions. Firmware, configuration, I/O behavior, communication, load response, and application compatibility still need to be reviewed.
What photographs should be included in a PLC spare request?
Send the nameplate, serial or revision markings, connector face, terminal blocks, mounting guides, cabinet position, adjacent modules, and any visible damage. Include a wider cabinet view when it helps identify the system role.
Should every refurbished module be tested in the original machine?
No. Direct testing in a live machine adds production and safety risk. Use an approved offline rack, simulator, or representative test environment whenever possible, then follow the site’s commissioning and change-control process.
What warranty should be requested?
Request a written warranty period, the covered failure modes, return or exchange process, exclusions, and any requirement to return the failed unit. Warranty length should be considered together with test evidence and traceability.
When should a plant reject an as-is spare?
Reject or quarantine it when the model identity is uncertain, the housing or connectors are damaged, storage exposure is unexplained, the test evidence is missing, or the application compatibility cannot be established for the intended use.
Turn inspection into recovery readiness
SmartNexMSK can help organize exact model evidence, condition requirements, test scope, configuration questions, and delivery targets for obsolete or hard-to-source automation parts. Send the model number, label photos, quantity, destination, and urgency to [email protected] or WhatsApp/Phone +86 18259474341.
Route this topic into a sourcing request
Connect the article topic to a model number, category, brand, quantity, and destination before opening the RFQ.
Related Insights
Continue with sourcing and model matching guides
 Sep 8, 2026
SANYO DENKI QS1E Spares: Save Parameters First
When a SANMOTION Q axis stops, the purchasing request often becomes a model number: “Please quote QS1E01AA0H4A3P1T.” That is a useful starting point, but…
Read guide Sep 6, 2026
Yaskawa SGDH-05DE-OY Spares: Check the Servo Chain
A servo drive fault often produces a deceptively simple purchasing request: “Replace the SGDH-05DE-OY.” In a running machine, however, the amplifier is only one…
Read guide Sep 5, 2026
GE IS220PCLAH1A Spares: Check Mark VIe Fit
When a Mark VIe cabinet develops an intermittent control fault, the urgent request often becomes a single line: “Please quote IS220PCLAH1A.” That is understandable…
Read guide